Table of Contents
Flange dimensions define more than the outside diameter of a metal ring. They establish how the component connects to the pipe, aligns with a mating flange, supports the sealing arrangement and fits into the available installation space. A drawing review must therefore follow the interfaces, rather than simply check that a few measurements look familiar. The costliest mismatch may be a small feature that was never included in the inquiry.
This guide explains how buyers and inspectors can organise flange dimensions into a useful review record. It covers drawing references, mating features, measurement planning and supplier clarification. It does not reproduce a standard dimension table or replace an approved drawing. Actual dimensions and acceptance tolerances must come from the applicable project documents and the specified product standard.
Identify the standard and component before reading flange dimensions
Check the drawing title, part number, revision and component type first. Record the nominal size, rating designation, facing and material identification. The same nominal size can appear in different dimensional systems or different types of flange. A measurement comparison without that context can appear correct while referring to the wrong family of components. Where a drawing uses abbreviations, resolve their meaning before sending it for manufacture.
ASME’s published B16.5 scope includes dimensional and tolerance requirements for the components it covers. The official ASME B16.5 description provides a starting point for checking scope; detailed flange dimensions must be taken from the specified edition and relevant component requirements. A supplier’s catalogue sketch should be reconciled with the purchase specification rather than accepted as the controlling drawing automatically.
Separate nominal size, outside diameter and bore
Nominal pipe size identifies a size designation, not every actual measured diameter. The flange outside diameter defines part of the external envelope. The bore relates to the internal opening or connected-pipe interface, where the flange type has one. These features serve different functions, and substituting one label for another creates ambiguity. A blind flange, for example, should not be treated as a weld-neck flange with an unspecified bore.
For a weld-end component, compare the relevant bore and end geometry with the ordered pipe and the approved joint detail. For a slip-on arrangement, check the pipe interface against the applicable drawing. A lap-joint arrangement requires attention to the stub end and backing flange as separate parts. When reviewing flange dimensions, follow the actual construction so the measurement sheet does not ask an inspector to verify features that the ordered type does not have.
Review the complete drilling pattern
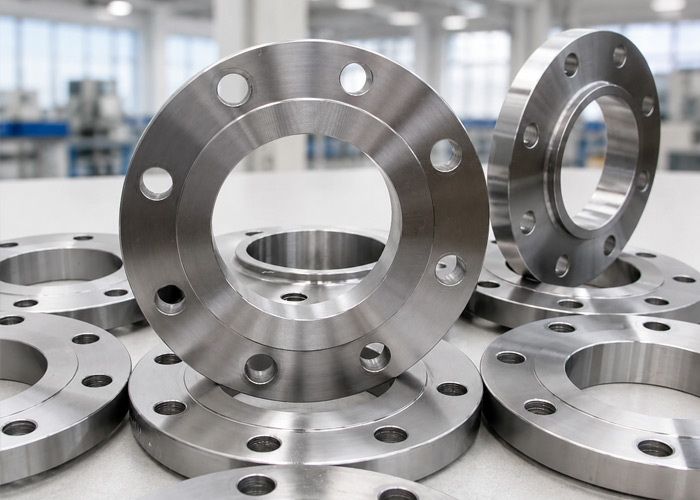
Record the bolt-hole count, hole diameter, bolt-circle diameter and any specified orientation. Hole count alone cannot establish a match. Two parts with the same number of holes may have different bolt circles or different hole sizes. The pattern must also be positioned relative to other drawing features where orientation matters. Include the mating component in the review rather than checking each part against a separate sketch with no interface comparison.
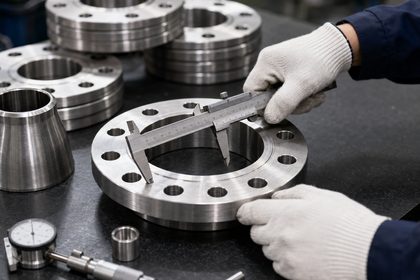
For replacement work, measure enough features to distinguish between plausible standards or variants. Photographs with a scale can support a survey but usually cannot establish acceptance dimensions because perspective, access and edge definition affect the result. Ask the surveyor to identify measurement points and equipment. If the pattern remains ambiguous, keep it as an unresolved engineering item; do not choose the closest catalogue pattern and rely on site modification.
| Feature | Why it matters | Record before release |
|---|---|---|
| Outside diameter | Installation envelope and external geometry | Drawing value, unit and tolerance reference |
| Bore or pipe interface | Compatibility with the connected pipe or mating part | Applicable type-specific dimensions and pipe data |
| Bolt-hole pattern | Fastener alignment across both components | Count, diameter, bolt circle and orientation |
| Facing geometry | Contact area for the selected sealing arrangement | Facing type, dimensions and condition requirements |
| Thickness and hub | Component geometry and available assembly space | Defined datums and applicable drawing requirements |
Use bolt-circle calculations as a survey cross-check
For equally spaced holes on a circle, the center-to-center chord between adjacent holes is related to the bolt-circle diameter by D = c / sin(pi / n), where c is the adjacent-hole chord and n is the number of equally spaced holes. This geometric relationship can help cross-check a survey when a direct center measurement is awkward. It assumes a circular, equally spaced pattern and correctly identified hole centers; it does not supply a flange-standard value.
As a purely illustrative example, eight equally spaced holes with a measured adjacent-center chord of 50 mm give a calculated circle diameter of about 130.66 mm. These numbers describe a hypothetical pattern, not an actual standard flange. Measurement uncertainty in the chord carries into the calculated result. Compare the finding with the controlled drawing and use an appropriate inspection method for final acceptance of flange dimensions.
Check the facing and gasket interface
Identify the facing type on both mating components and the sealing arrangement that the project requires. Review the relevant contact geometry and any specified surface finish. A raised face, flat face or ring-joint arrangement cannot be treated as an interchangeable visual detail. The gasket and the mating surface must be considered together. If a quotation changes the facing, obtain a technical disposition before accepting it.
Separate dimensional conformity from surface condition. A face can have the required nominal geometry and still carry damage, contamination or an unacceptable surface feature. Define what the inspector must measure, what must be visually examined and which document supplies the acceptance basis. Protect the contact surfaces after inspection. The flange dimensions report should identify the feature and its result without implying that a dimensional check alone establishes sealing performance.
Define thickness, hub and overall-length datums
A thickness or length value is meaningful only when its start and end surfaces are clear. Check how the drawing treats the facing and where the measurement datums are located. For a hubbed component, identify the hub dimensions and weld-end references relevant to the purchase. A supplier and buyer can report different values for the same part if they use different reference surfaces, even when both believe they are checking flange dimensions correctly.
Ask for a drawing clarification when a feature is shown but not dimensioned, or when two dimensions conflict. Avoid solving the discrepancy by measuring a scaled print or estimating from a website image. Record the accepted clarification through the drawing revision or an approved technical query. An agreed datum definition also helps the receiving inspector repeat the supplier’s measurement and investigate differences without starting the review from scratch.
Keep units and tolerances visible
Confirm whether the drawing controls dimensions in millimetres, inches or another stated basis. A conversion displayed for convenience should not silently become a second acceptance value. Check whether individual tolerances, general drawing tolerances or a referenced standard govern each feature. Where the project uses several documents, define the precedence that resolves a conflict. Do not let the inspection team invent a tolerance because a nominal value appears on the sheet.
Select measurement equipment suitable for the feature and required tolerance. Record the equipment identity and its calibration status under the project’s inspection system. Large dimensions, hard-to-reach surfaces and hole-center measurements may need different methods from a simple external diameter check. The flange dimensions report should state the actual result in the correct unit and retain the acceptance basis, rather than reduce every reading to an unexplained tick mark.
Create an auditable flange dimensions report
Give each inspected item or defined inspection lot a traceable identity. The report should list the order reference, part or heat identification as applicable, drawing revision, feature description, nominal requirement, tolerance reference, measured value, unit and disposition. Add the inspection date and responsible person. If the agreed plan uses sampling, identify the sample and sampling basis instead of implying that every delivered part was measured.
Use a separate comment field for observations such as limited access, a measurement method change or an unresolved drawing query. Link any nonconformity to the affected item and feature. An inspector should be able to show which requirement was not met and how the item was dispositioned. A report that says all dimensions acceptable without a defined scope offers much less evidence than a concise, feature-based record.
Investigate mismatches before altering the part
When flange dimensions do not match, first verify identity, drawing revision, units and measurement method. Confirm whether the supplied component is the ordered type and standard. Then compare the actual readings with the mating part and the controlling requirements. This sequence separates an identification error, a survey error, a document conflict and a manufacturing discrepancy, each of which calls for a different response.
Do not enlarge holes, machine a sealing face or force alignment as an informal way to make a part fit. Such changes can affect the component and the approved design. Record the discrepancy, protect the item and obtain an authorised disposition. If rework is accepted, define the revised requirements and repeat the affected inspection. Keep the original and final records connected so a later reviewer can understand what was changed and why.
Transfer the accepted dimensional basis to fabrication
The fabrication team needs the accepted drawing and interface information, not only a supplier’s commercial description. Provide the relevant pipe data, orientation details, joint references and approved deviations. If the component is intended for a replacement, include the field-survey basis and any remaining site checks. This handover helps prevent a correctly manufactured flange from being installed against an outdated arrangement.
Keep the dimensional baseline under revision control through ordering, inspection and assembly. A change to the connected equipment, pipe wall or facing should trigger a review of the affected flange dimensions. Close the purchasing record only when the delivered identity, measurement evidence and accepted interface requirements agree. That disciplined document trail is often more valuable than collecting a long list of measurements without knowing which drawing controls them.
For the listed product range, review Flange Assembly and drawing-based customization support. Provide the actual interface requirements for confirmation in the quotation.
Send your controlled drawing and mating-component information through the form below for a quotation review. Include the nominal size, standard, rating, facing, material, required flange dimensions, quantity and any inspection-report requirements. For replacement work, attach the field-survey reference and identify dimensions that still need confirmation.
Frequently Asked Questions
Which flange dimensions are essential for checking a mating connection?
Review the applicable bore or pipe interface, drilling pattern, facing, thickness and installation envelope. The precise feature list depends on the flange type and controlled drawing.
Is nominal pipe size the same as the flange outside diameter?
No. Nominal size is an identification designation. The actual outside diameter and other dimensions must be obtained from the applicable drawing and standard.
Can a photograph establish flange dimensions for acceptance?
A photograph can support identification or a field survey, but perspective and uncertain reference points limit its measurement value. Use an agreed inspection method for acceptance.
Does the bolt-hole count prove two flanges will mate?
No. Bolt-circle diameter, hole diameter, orientation, facing and the other relevant interface requirements must also agree.
What should happen when delivered flange dimensions differ from the order?
Verify identity and the measurement basis, record the affected feature and obtain an authorised disposition. Do not modify the part informally to make it fit.