İçindekiler Tablosu
Flange inspection is most effective when the buyer defines the evidence before manufacturing begins. An inspector cannot reconstruct an incomplete purchase specification at the end of production, and a certificate package cannot answer a question that was never included in its scope. The inspection plan should connect each ordered requirement to a defined check, an acceptance reference and a record that identifies the affected component or lot.
This flange inspection guide helps industrial buyers and quality teams build that connection. It separates document review, identity checks, dimensional measurement, surface examination and any additional testing required by the order. It also explains how to record deviations and release decisions. The actual acceptance criteria must come from the controlled purchase documents, applicable standards and approved project requirements.
Establish the controlling flange inspection documents
Start with the purchase order, accepted quotation, technical specification, drawing revisions and approved deviations. Confirm the component type, size, standard, rating designation, facing and material requirements. List supplementary requirements separately so they do not disappear inside a general description such as full inspection. Where documents conflict, obtain a formal clarification of precedence before work is released.
Record the references in the inspection plan and identify which revision controls each check. ASME’s official B16.5 scope includes marking and testing among its covered subjects. Detailed acceptance requirements must still be taken from the applicable edition and order. A standard reference should lead to a defined check, rather than appear as an unsupported statement of conformity on the final report.
Agree the inspection stages and release responsibilities
Define which activities are completed by the manufacturer, reviewed by the buyer or attended by an appointed inspector. Identify hold points, witness points and document-review points according to the agreed inspection system. State how much notice is required for attendance and what happens when a point cannot be witnessed. These commercial and quality arrangements should be settled before production reaches the relevant stage.
The flange inspection plan should also identify who may accept a deviation and who may authorise shipment. An inspector’s observation and an engineer’s disposition are different decisions. Keep the responsibilities clear when a result falls outside the requirement or when an agreed record is missing. A shipment release should not be inferred from silence or from the fact that the finished components have already been packed.
Connect material documentation to the delivered parts
Review the material documents against the ordered specification and grade. Check that the required results and identification information are present for the agreed document scope. Then verify how the heat, lot or other accepted identity connects to the physical flange. A certificate that cannot be linked to the delivered items does not provide the intended traceability, even if its individual values appear plausible.
Traceability should remain usable through manufacturing and packing. Ask how identity is transferred when material is processed and how finished parts are segregated where several grades or heats are handled together. If the order requires individual identification, verify that requirement explicitly. Flange inspection should produce a coherent relationship between the order line, part marking, material record and shipment identity.
Verify marking and physical identification
Compare the required markings with the applicable product and purchase requirements. Record enough information to identify the item and its technical basis during receiving and later fabrication. Check that the marking is readable and that the method and location do not conflict with the specified condition of the component. If a marking is missing or unclear, determine its significance before release rather than ask the receiving team to infer the identity from appearance.
Photographs can support the flange inspection record when they clearly show the part identity and the feature being discussed. Use a consistent reference so the image can be linked to the inspection report. A large folder of unlabelled photographs is difficult to audit. Retain the actual observation and disposition in the report; the photograph should illustrate that evidence rather than replace the inspector’s description.
Measure the dimensions that control the interfaces
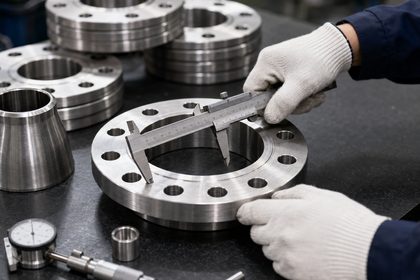
Build the dimensional checklist from the actual flange type and drawing. Relevant features may include outside diameter, thickness, drilling, facing, bore, hub and weld-end geometry. Do not use the same unchecked feature list for every type. A blind flange, a weld-neck flange and a lap-joint backing flange present different interfaces. Identify the datums and units so that the supplier and receiving inspector can repeat the measurement meaningfully.
For each measured feature, retain the requirement, tolerance reference, actual result and disposition. Record the measuring equipment under the quality system’s requirements. If the plan permits sampling, state the defined lot, selected sample and agreed sampling basis. Avoid reporting a full batch as dimensionally inspected when only a sample was measured. The flange inspection scope should remain evident to the person making the release decision.
| Inspection area | Evidence to request | Question before acceptance |
|---|---|---|
| Material identity | Required material record linked to heat or lot | Can the documentation be traced to these delivered parts? |
| İşaretleme | Recorded identification and applicable marking review | Are the required markings present and readable? |
| Dimensions | Feature-based report with units and acceptance references | Were the critical mating features checked to the controlling drawing? |
| Yüzey durumu | Recorded condition and disposition of observed defects | Do the contact and functional surfaces meet the specified basis? |
| Additional examination | Approved method, coverage and report references | Does the actual work match the examination ordered? |
| Release | Closed deviations and accepted shipment package | Who has authorised shipment and what remains open? |
Review sealing faces and other functional surfaces
Examine the specified contact surfaces for visible damage, contamination and other conditions relevant to the acceptance basis. Keep geometric conformity and surface condition as separate observations. A component may meet its dimensional requirement while having a damaged sealing area, or present a clean appearance while a critical dimension is wrong. The inspection plan should tell the reviewer which condition checks are required and how findings are dispositioned.
Where a surface finish requirement applies, agree the method and reference used to evaluate it. Do not assign a numerical finish from a photograph or visual impression. If repair or re-machining is proposed, obtain the appropriate authorisation, preserve traceability and repeat the affected checks. Protect accepted faces during the remaining handling and packing activities so the condition recorded during flange inspection remains relevant at shipment.
Specify additional tests and examinations precisely
Additional examination may be required by the material specification, product requirements or project order. Define the method, extent, acceptance reference, personnel requirements where applicable and report contents. The expression all tests included is too vague for comparable quotations or an auditable release. State the required scope before manufacture so the supplier can plan access, sequence and witness activities.
Distinguish material testing, component examination and system testing after installation. A report for one activity should not be treated as evidence for another. Do not assume every individual flange is hydrostatically tested simply because a product description refers generally to testing. Ask the supplier to identify the actual applicable requirements and the evidence offered. Escalate any scope difference for technical review rather than silently broaden the meaning of a certificate.
Manage nonconformities without losing the original requirement
When a result does not meet the requirement, identify the affected component or lot and record the specific discrepancy. Preserve the original acceptance reference and the actual observation. Separate the finding from the proposed disposition: rework, replacement, concession or another authorised action must be reviewed by the appropriate owner. A supplier’s explanation does not by itself close a nonconformity.
If rework is approved, define what changes and which inspections must be repeated. Retain the original and final evidence under the same traceable record. Where a concession is accepted, state its limits and authorisation clearly enough for receiving and fabrication teams to understand. Flange inspection loses value when a report is rewritten to look clean without showing how an out-of-requirement condition was handled.
Inspect preservation, packing and shipment identity
Check the packing requirements against the transport and receiving plan. Protect the functional surfaces, keep identification readable and prevent items from moving in a way that causes damage. Where several order lines, sizes or material identities share a shipment, use clear segregation and package labels. Confirm that the packing list identifies the contents in a form the receiving team can reconcile with the purchase order.
Photograph the agreed packing condition when the inspection plan calls for it, and link the evidence to the package references. Record any items packed separately and identify where the corresponding documents will be provided. Flange inspection should end with a shipment that preserves the accepted product and its identity. An accurate dimensional report offers limited practical value if transit damage or mixed identification prevents the buyer from using the delivered parts.
Release the shipment with a complete evidence package
Review the final inspection status, material documents, dimensional results, additional examination records, packing evidence and deviation register. Confirm that each required activity has either been completed or has an explicit authorised disposition. The release record should identify who made the decision, the scope released and any conditions that remain for receiving or installation. Keep actual completion separate from a proposed shipment date.
Provide the receiving team with the accepted order references and an organised document index. They should be able to verify quantity, identity, condition and the required evidence without searching an unrelated correspondence archive. Retain the flange inspection package with the project records for future fabrication, maintenance or investigation. The result is an auditable link from an agreed purchase requirement to a specific delivered component and a clear release decision.
Listelenen ürün yelpazesi için inceleyin Flanş Montajı ve çizim tabanlı özelleştirme desteği. Teklifte onay için gerçek arayüz gereksinimlerini sağlayın.
Define the required flange inspection scope with your next inquiry. Use the form below to provide the flange specification, drawing revision, quantity, certificate requirements, critical dimensions and any witness or hold points. Include the delivery destination and document timing so the proposed supply and inspection scope can be reviewed together.
Sıkça Sorulan Sorular
When should the flange inspection plan be agreed?
Before manufacturing begins. Early agreement allows the supplier to plan the required checks, document collection, notice periods and witness or hold points.
Does a material certificate complete flange inspection?
No. Material documentation is one part of the evidence. Identity, dimensions, surface condition and any additional ordered checks must also be addressed within the agreed scope.
Can a sample inspection be reported as inspection of every flange?
No. Identify the lot, selected sample and agreed sampling basis. Keep the inspected scope visible in the report and release decision.
What should a flange inspection report say about a deviation?
State the affected identity, original requirement, observed result, proposed action, authorised disposition and any repeated inspection after rework.
Is shipment release the same as installed-system acceptance?
No. Shipment release concerns the agreed supply scope. Installation, system testing and commissioning have their own requirements and responsible parties.